Just let me clarify this: This wasn't meant to be a two-part story, but I guess life (and engineering problems) have a funny way of caring about your plans.
Step one: In order to have full adjustability on all three carbs I wanted to convert the center carb to an adjustable linkage as well. Unfortunately the fixed one is drilled slightly different and can't be fitted. So a new shaft had to be made: one 10mm ally bar
Make a nice snug fit 5mm center punch to mark the shaft precisely.
The punch marks are a lot more visible of the area has been marked with a felt pen.
I decided against the stock pin-setup for the throttle butterfly, which in turn meant making some room for the bolt head on the mill.
And as it didn't matter anymore anyway, I picked up some 15x15x2mm stainless angle bar and make a new set of rails for the carbs.
Final install and sync on the bike. (And yes, I am still waiting for the 6mm banjos, but other than that it's done.)
A first jetting at #20, #137.5 revealed it running rich on the top end, so after a slight rejet to #20, #125 that's definitely usable for the moment. Maybe a #22.5 pilot and half a turn less on the mix screw, but that's something for another day...
Sunday, 8 April 2018
Sunday, 1 April 2018
The XS Triple Sidecar - modifying flatslides to fit
If you're running one of the more common bikes, you simply buy a set of flatslide carbs second hand, slap 'em on and there's probably even some info out there on how to jet them so you at least have a point to start. But I wanted a triple.
First step was to get the spacing right. As you can see these carbs are spaced pretty tight already. (At least #1 and #2 are.) In order to do that the old carbs had to come off and I had to take some measurements.
It became apparent that the only way to make this work would be by moving the fuel inlets on the two outer carbs to the outside, as each pair of carbs had to be spaced more than 25mm closer together and at the very most seven or eight mm would have been possible. Luckily the castings were all identical, just drilled according to the individual requirement. As such it was just a matter of drilling out the fuel passage from the other side and then thread both sides.
In order to gain another nine milimetres, the casting boss was milled flush with the carb body.
As there wasn't enough meat to tap the carb bodies in M8x1.00, I had to make three adaptors to use some industrial/hydraulic Lego.
Testfitted the carbs onto the engine. As I have used this type of carbs before on the XS400 RatRacer, I still had a piece of throttle shaft left over, which I used to straighten out the carbs and have them sit as perfectly straight as I could to prevent binding later on.
Quickly tacked the rails together for a test-fit.
And then re-tap (M4) the throttle shaft to accomodate for the new spacing.
And then shorten the throttle shaft on the lathe. (Did I mention, that I got myself a MGEHR16 parting tool? It's the dog's d*ngl**s...)
Sorting out the choke linkage was a beautifully simple job, as it only meant to cut a bit of 4mm stainless rod to length and tighten up the hooks of the choke setup.
Installed and looking d*mn sexy.
They say that every great triumph needs a bit of tragedy.
This one needed a bit of re-engineering. The solution will be found in the next post.
(Oh and yes, the VM36s will be for sale, once they received a half-decent cleanup.)
First step was to get the spacing right. As you can see these carbs are spaced pretty tight already. (At least #1 and #2 are.) In order to do that the old carbs had to come off and I had to take some measurements.
It became apparent that the only way to make this work would be by moving the fuel inlets on the two outer carbs to the outside, as each pair of carbs had to be spaced more than 25mm closer together and at the very most seven or eight mm would have been possible. Luckily the castings were all identical, just drilled according to the individual requirement. As such it was just a matter of drilling out the fuel passage from the other side and then thread both sides.
In order to gain another nine milimetres, the casting boss was milled flush with the carb body.
As there wasn't enough meat to tap the carb bodies in M8x1.00, I had to make three adaptors to use some industrial/hydraulic Lego.
Testfitted the carbs onto the engine. As I have used this type of carbs before on the XS400 RatRacer, I still had a piece of throttle shaft left over, which I used to straighten out the carbs and have them sit as perfectly straight as I could to prevent binding later on.
Quickly tacked the rails together for a test-fit.
And then re-tap (M4) the throttle shaft to accomodate for the new spacing.
And then shorten the throttle shaft on the lathe. (Did I mention, that I got myself a MGEHR16 parting tool? It's the dog's d*ngl**s...)
Sorting out the choke linkage was a beautifully simple job, as it only meant to cut a bit of 4mm stainless rod to length and tighten up the hooks of the choke setup.
Installed and looking d*mn sexy.
They say that every great triumph needs a bit of tragedy.
This one needed a bit of re-engineering. The solution will be found in the next post.
(Oh and yes, the VM36s will be for sale, once they received a half-decent cleanup.)
Wednesday, 28 March 2018
Project overview 2018
As I got caught by a bit of the old manflu, I thought it may not be the worst idea to come up with a project plan for 2018.
Sidecar:
Sidecar:
fit the TM33 flatslides (I've got all the parts, so that'll hopefully be the next project, but it requires salt-free roads, as the bike most likely will be out of service for a few days)fight the rust- alter the rear subframe a bit, so the mufflers can be angled up a bit mor, so to be able to remove the rear wheel without taking the mufflers off
- fit a new front mudguard (needs sandblasting and paint)
- fit LED bulbs in both tail-lights
- Finish that new engine:
decide whether to move to the other set of engine cases I haveor not, improve on some of the past work, reshape the combustion chambers, install the BT1100 crank, shorten the cylinders and finally assemble everything and install) - alter the speedo illumination, so I can run two LEDs on the inside: one on the top, one on the bottom (same as on the XS-hack)
- build a new 2in1in2 exhaust with a better collector
- new pannier-rack
- swap the yokes and also check the fork tubes for straightness
- Get it running and then sell it - more on that very soon
- swap the handlebars
- finish the carb swap to the later model (needs a new choke-cable)
- install the pannier rack and see where it needs tweaking
- fit the XT550 headlight
- convert to 600cc
sell the turbo-kit- build a second turbo-kit from leftovers based on the GT15
- fit the supercharger
- burn some tyres
- try to legally register it overhere
- build a fly-cutter for skimming the TR1 cylinder heads
- build a fixture to use the above 😉
- build a proper belt sander as the small one I have right now is pretty useless
- fit the DRO to the mill's quill
- build my own version of the fog-buster (mist cooling) for my mill
- build the tube sander
- rebuild the lathe-spindle and feeds
- build a set of starter rollers
rebuild the spindle on the drillpress
Sunday, 25 March 2018
XT600 engine rebuild - finished ... not. (part 4)
Don't you hate those stories that seemingly only consist of cliffhangers? Well, me too.
I picked up where we last left off and that was by installing the primary gears and timing the counterbalancer.
As the old piston was still fine, only new rings were installed and the piston thouroughly cleaned.
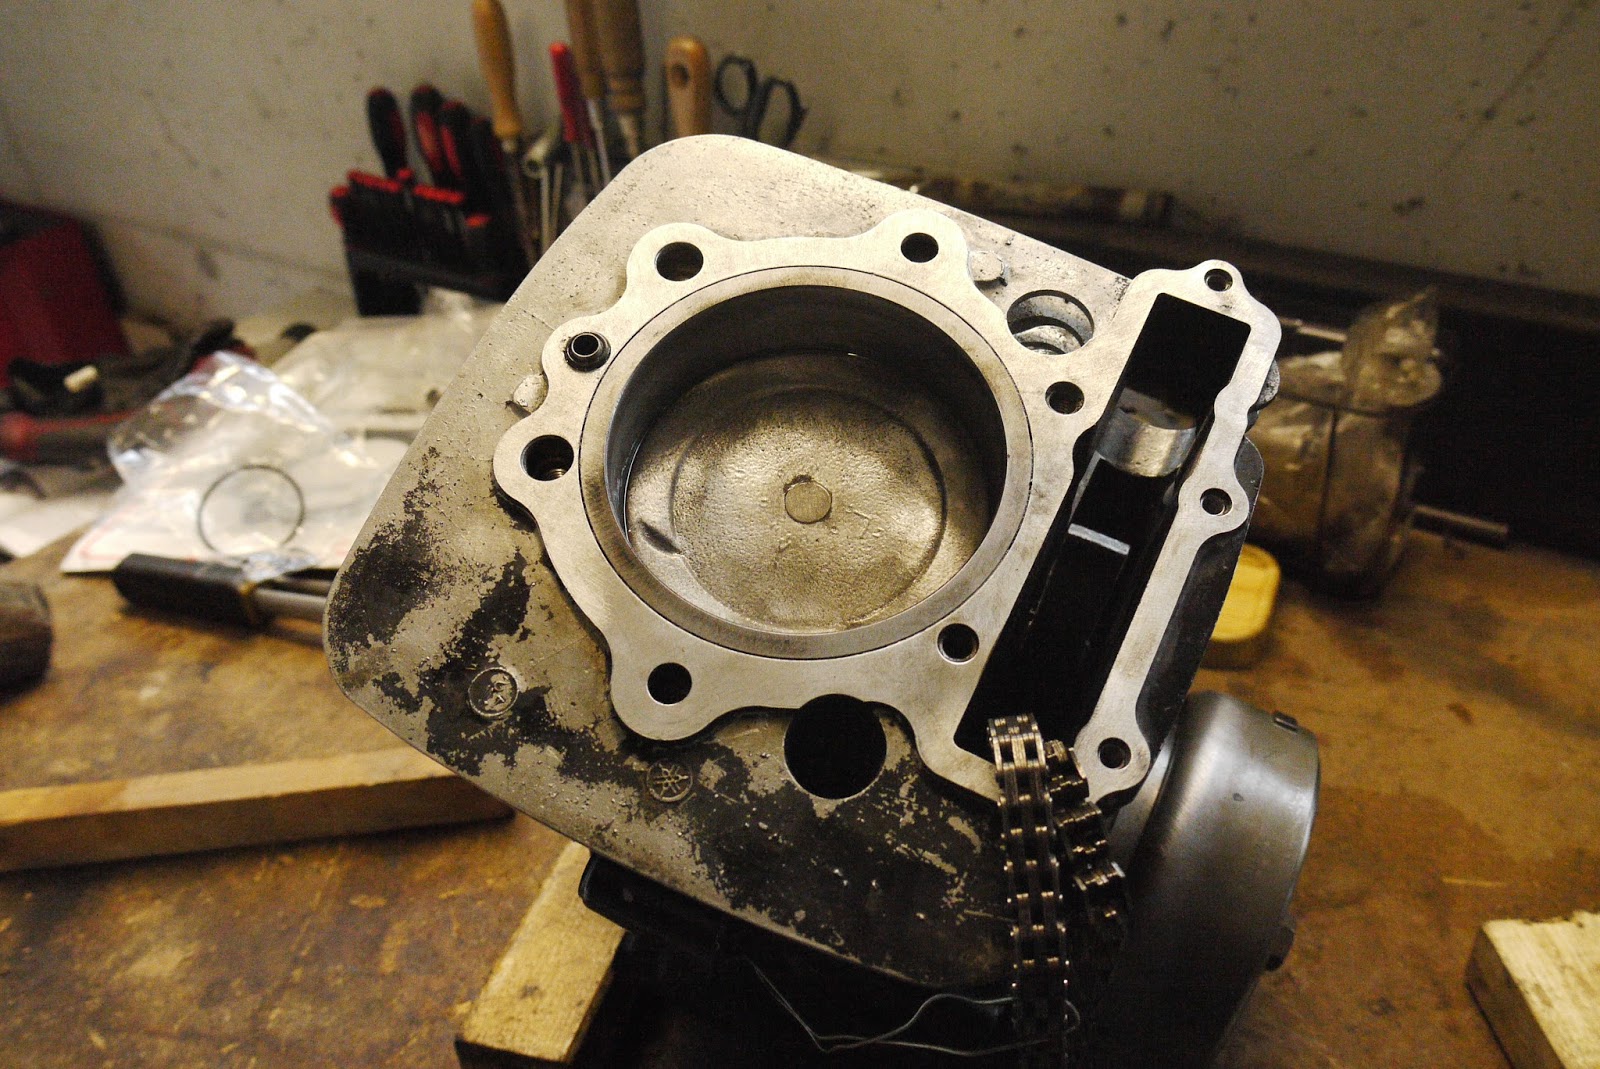
The cylinder was given a quick once over with the three-legged hone in order to give the new rings something to bite into and both top and bottom were cleaned with chemical gasket remover and a rotating nylon brush.
The combustion chamber needed a bit more cleaning as a lot of old oil, most likely caused by the stuck oil-scraper ring, had deposited on the valves.
The rockers are in like new shape.
Cam installed and timed up.
Some MOS2-based lube was used as assembly lube, as the engine will probably sit a couple more days and weeks until it is fired up the first time.
As valve adjustment is significantly easier with the engine out of the frame, it was done on the bench.
... and there you have it: The engine is ready for install.
Except for the fact that we swapped the gearbox for one out of a later model and so the clutch center has got a different spline.
I picked up where we last left off and that was by installing the primary gears and timing the counterbalancer.
As the old piston was still fine, only new rings were installed and the piston thouroughly cleaned.
The cylinder was given a quick once over with the three-legged hone in order to give the new rings something to bite into and both top and bottom were cleaned with chemical gasket remover and a rotating nylon brush.
The combustion chamber needed a bit more cleaning as a lot of old oil, most likely caused by the stuck oil-scraper ring, had deposited on the valves.
The rockers are in like new shape.
Cam installed and timed up.
Some MOS2-based lube was used as assembly lube, as the engine will probably sit a couple more days and weeks until it is fired up the first time.
As valve adjustment is significantly easier with the engine out of the frame, it was done on the bench.
... and there you have it: The engine is ready for install.
Except for the fact that we swapped the gearbox for one out of a later model and so the clutch center has got a different spline.
Tuesday, 20 March 2018
Repurposing an old boring bar for boring head use on the mill
Chinese boring heads receive a terrible amount of bad press and compared to some German precision tooling from a company starting with W**********, they aren't even worthy to be considered as sh*te. That being out of the way, when the price-point (new) sets you apart roughly by the factor of 100, you may expect or accept (depending on the point of view) slight variations in quality and finish.
Now that we've established that these boring heads are somewhat inferior to their European counterparts, it is quite safe to assume, that the actual boring tools with their brazed on carbide are equally challenged. And this is where this post comes in. I used to have an old boring bar with TNMG16 insert that for many reasons, the main one being that the new one required a smaller pilot hole as it has no top-support of the insert, was swapped out for a TCMT16-tool on the lathe.
Now the old tool had a 20mm shaft, milled down top and bottom to 16mm, so it was necessary to turn it down to 12mm to fit into the boring head.
Fit it into the boring head and tighten the locking screw VERY tight once so you have a mark.
Also while I was at it, all the Chinesium set screws were replaced with genuine 8.8 stuff from my local hardware store.
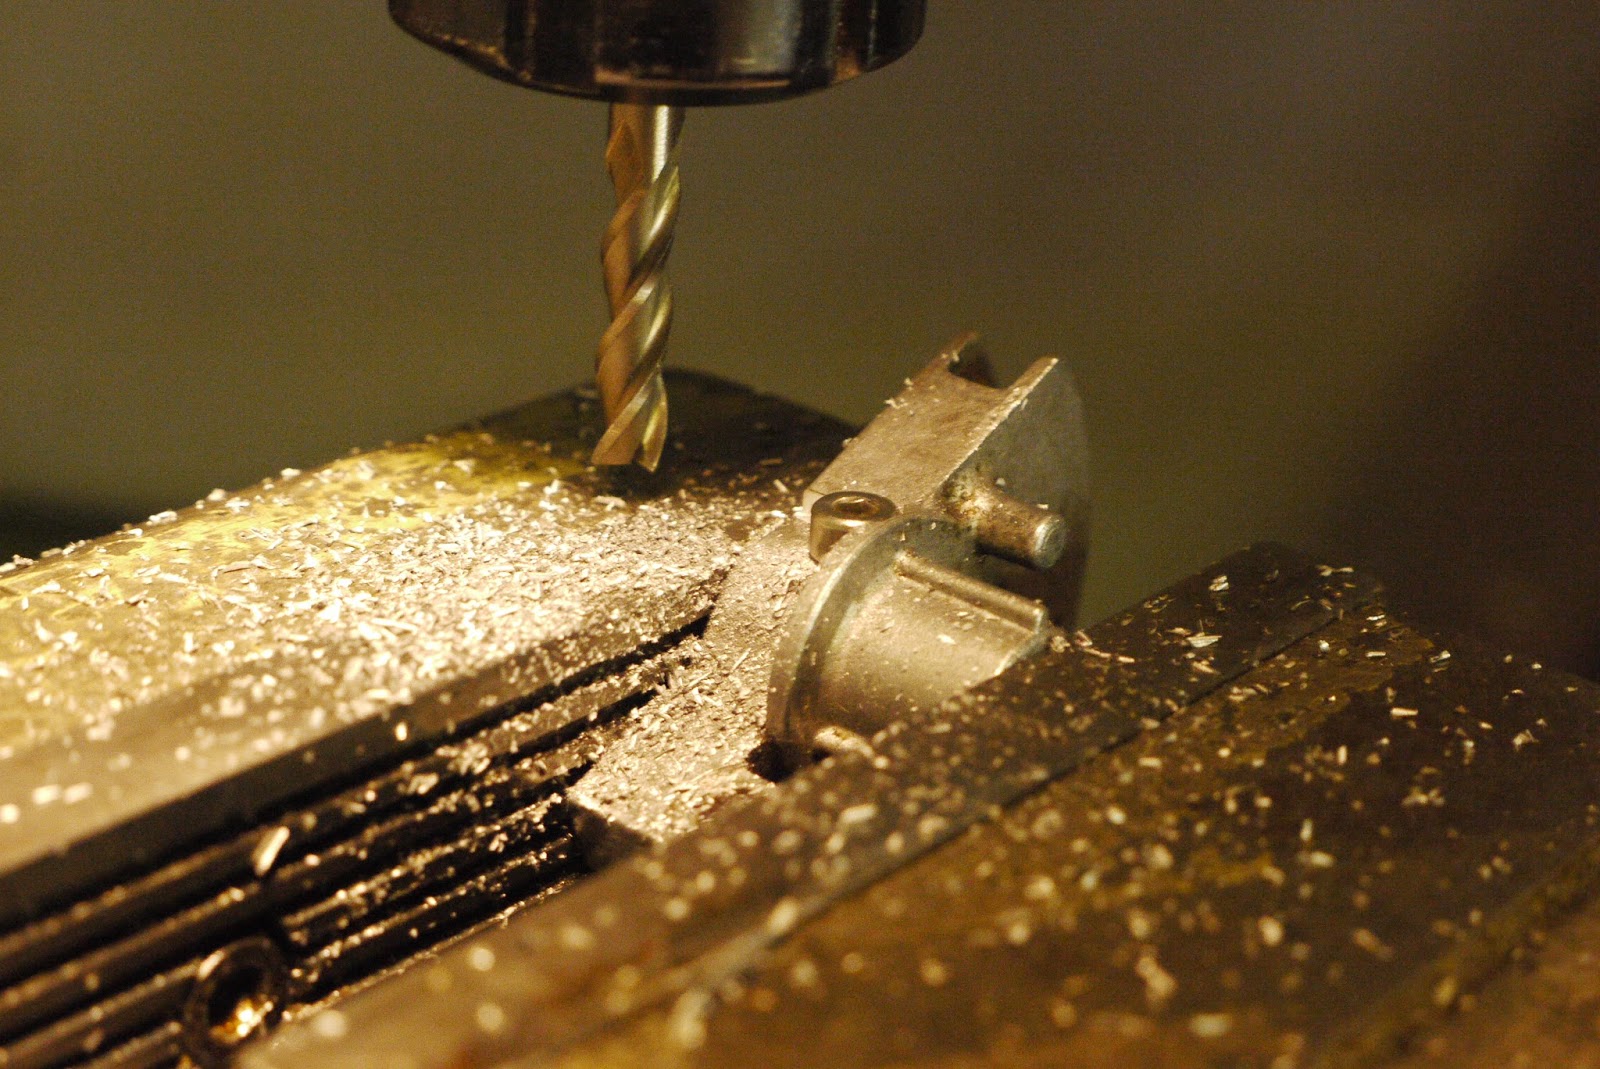
Then just quickly run over that mark with the 6mm endmill and make a nice flat, so that even in the unlikely case of the set-screw coming loose, I don't end up with the boring bar flying through the room.
And the final article. This should have enough length to bore XV or XT engine cases without removing the case studs, should the need arise.
And compared to the old tooling, which had a 12mm shank, but then tapered down to approx 6mm, this should be a lot beefier resulting in nicer cuts.
Now that we've established that these boring heads are somewhat inferior to their European counterparts, it is quite safe to assume, that the actual boring tools with their brazed on carbide are equally challenged. And this is where this post comes in. I used to have an old boring bar with TNMG16 insert that for many reasons, the main one being that the new one required a smaller pilot hole as it has no top-support of the insert, was swapped out for a TCMT16-tool on the lathe.
Now the old tool had a 20mm shaft, milled down top and bottom to 16mm, so it was necessary to turn it down to 12mm to fit into the boring head.
Fit it into the boring head and tighten the locking screw VERY tight once so you have a mark.
Also while I was at it, all the Chinesium set screws were replaced with genuine 8.8 stuff from my local hardware store.
Then just quickly run over that mark with the 6mm endmill and make a nice flat, so that even in the unlikely case of the set-screw coming loose, I don't end up with the boring bar flying through the room.
And the final article. This should have enough length to bore XV or XT engine cases without removing the case studs, should the need arise.
And compared to the old tooling, which had a 12mm shank, but then tapered down to approx 6mm, this should be a lot beefier resulting in nicer cuts.
Friday, 16 March 2018
XT600 engine rebuild - completing the shortblock - once more (Part 3)
Ever had a deja-moo? The feeling, you've seen this b*llsh*t before? Don't worry, you haven't gone a bit soft in the old headroom, but here we are, doing exactly the same job once more as the #3 selector fork was slightly bent.
Using the right chemicals cleaning the gasket goo off was a matter of simply wiping it off.
Gearbox back in.
Using a different selector drum and forks.
Not even remotely as much liquid gasket required as you'd think.
... and back together.
All in all about one hour of work and an hour well spent as now the gearbox is as smooth as I like it to be.
Using the right chemicals cleaning the gasket goo off was a matter of simply wiping it off.
Gearbox back in.
Using a different selector drum and forks.
Not even remotely as much liquid gasket required as you'd think.
... and back together.
All in all about one hour of work and an hour well spent as now the gearbox is as smooth as I like it to be.
Wednesday, 14 March 2018
The Turbo TR1 - maintenance
Judging by backlog, the last time I worked on the Turbo TR1 was in January over a year ago.
As I admittedly have plans of making this work again this year and also have a rather nice (in my book at least) idea on how to tackle the boost-crisis, it wasn't out of place to do some maintenance.
So that's what the brake fluid looked like when it came out. Mind you, this bike hasn't been driven a single mile in 2017.
This is actually Everyday TR1's brake pump (as identifiable by the mirror), so did those brakes too. Oh and while I was at it, found out that the old brakepump on the Turbo is on its last legs, so a "new one" (14mm) has been ordered.
While I was at it, I also (finally) fitted a left over lower clutch cable cover and some new (to me) solid handle-bar holders as the bar-mount rubbers are well past it.
So what's hot and cooking for this old girl?
That's a Volkswagen-branded Eaton M24 out of a 1.4TSI Polo. Now I hear you say, 24? that means it will only displace 24ci per revolution, doesn't that mean you're going to spin the living cr*p out of it? Well, you see that snout? It's got 1.93:1 step up gears on it, essentially turning it into a blower that displaces 46,3 ci per revolution. Why put that in, instead of the M45, I used to have? Simple packaging really. The M45 just wouldn't fit in between the front of the engine and the frontwheel.
Excited? Me too.
As I admittedly have plans of making this work again this year and also have a rather nice (in my book at least) idea on how to tackle the boost-crisis, it wasn't out of place to do some maintenance.
So that's what the brake fluid looked like when it came out. Mind you, this bike hasn't been driven a single mile in 2017.
This is actually Everyday TR1's brake pump (as identifiable by the mirror), so did those brakes too. Oh and while I was at it, found out that the old brakepump on the Turbo is on its last legs, so a "new one" (14mm) has been ordered.
While I was at it, I also (finally) fitted a left over lower clutch cable cover and some new (to me) solid handle-bar holders as the bar-mount rubbers are well past it.
So what's hot and cooking for this old girl?
That's a Volkswagen-branded Eaton M24 out of a 1.4TSI Polo. Now I hear you say, 24? that means it will only displace 24ci per revolution, doesn't that mean you're going to spin the living cr*p out of it? Well, you see that snout? It's got 1.93:1 step up gears on it, essentially turning it into a blower that displaces 46,3 ci per revolution. Why put that in, instead of the M45, I used to have? Simple packaging really. The M45 just wouldn't fit in between the front of the engine and the frontwheel.
Excited? Me too.
Subscribe to:
Posts (Atom)